

Carbide drill series – Geppetto Cutting Tools
Geppetto Cutting Tools solid carbide drills: internal and external coolant in 3xD, 5xD and 8xD lengths, NC spot drills, centre and step drills. From Ø1 to Ø20, with catalogue cutting data.
A carbide drill is ground entirely from sintered tungsten carbide and runs at much higher cutting speeds and longer tool life than HSS drills. Geppetto Cutting Tools manufactures carbide drills on a CNC tool grinding machine; drill diameter is ground to m7 and shank diameter to h6. The right drill is chosen by hole depth (3xD, 5xD, 8xD), machine coolant capability, workpiece material and required hole quality.
Carbide drill types
- Internal coolant carbide drills: D32 (3xD), D52 (5xD), D82 (8xD) Ø3–Ø20; DT50 and DT80 Ø1–Ø2.9 for small diameters.
- External coolant carbide drills: D30 (3xD) and D50 (5xD) Ø3–Ø20.
- Spot and centre: NC90 spot drills Ø5–Ø20, DC carbide centre drills Ø0.5–Ø6.3.
- Step drills: D181 and D181F short 90° step drills Ø2.5–Ø14; special step drills to drawing.
- Special materials: DK series for Kevlar, straight-flute DSF series.
Get a quote / Send a drawing
Subject: Carbide drill series – Geppetto Cutting Tools. Message us on WhatsApp or by e-mail and attach your drawing or a dimensioned sketch. The product/page name is added automatically – just add material, size and quantity.
- 1Drawing or dimensions
- 2Material and quantity
- 3Quote and feasibility reply
Internal or external coolant?
On internal-coolant carbide drills (D32, D52, D82, DT50, DT80) coolant reaches the tip through channels in the tool. It cools the cutting zone and pushes chips out of the flutes. For 5xD and deeper holes, long-chipping materials such as stainless steel, and high-feed production, internal coolant is the first choice – provided the machine has through-spindle coolant.
If the machine has no through-spindle coolant, use external-coolant D30 and D50. Aim nozzles at the tip and use peck cycles in deep holes to avoid chip packing.
Coating and material choice
Standard series use AlTiN coating. AlTiN offers high heat resistance and works well in steel, alloy steel, stainless steel and cast iron. For Kevlar and composites, sharp uncoated or AlCrN-coated DK and DSF series are preferred. For aluminium and non-ferrous metals, uncoated or suitably coated special drills can be made.
What to watch when choosing a carbide drill
Divide hole depth by diameter: up to 3xD a short drill is stiffer and gives better hole quality. Do not choose a longer drill than needed. In deep holes, a short pilot of the same diameter extends life. Use a low-runout hydraulic or shrink holder; runout is the carbide drill’s worst enemy. Start from catalogue cutting data and use our calculator for speed and feed. Worn carbide drills can be reground to original geometry with our regrinding service.
Compare the series
| Series | Diameter | Z | Coating | Cutting data · ISO P | Cutting data · ISO M |
|---|---|---|---|---|---|
| D32 (Z2)3xD, internal coolant | Ø3 - Ø20 | 2 | AlTiN | – | – |
| D52 (Z2)5xD, internal coolant | Ø3 - Ø20 | 2 | AlTiN | – | – |
| D82 (Z2)8xD, internal coolant | Ø3 - Ø20 | 2 | AlTiN | – | – |
| DT50 (Z2)5xD, internal coolant | Ø1 - Ø2.9 | 2 | AlTiN | – | – |
| DT80 (Z2)8xD, internal coolant | Ø1 - Ø2.9 | 2 | AlTiN | – | – |
| D30 (Z2)3xD, external coolant | Ø3 - Ø20 | 2 | AlTiN | – | – |
| D50 (Z2)5xD, external coolant | Ø3 - Ø20 | 2 | AlTiN | – | – |
| NC90 (Z2)NC spot drills | Ø5 - Ø20 | 2 | AlTiN | – | – |
| D181 (Z2)Short solid carbide 90° step drill | Ø2.5 - Ø14 | 2 | Uncoated | – | – |
| D181F (Z2)Short solid carbide 90° step drill | Ø2.5 - Ø14 | 2 | AlCrN | – | – |
| DC (Z2)Carbide centre drill | Ø0.5 - Ø6.3 | 2 | Uncoated | – | – |
| DK (Z2)Drills for Kevlar | Ø3 - Ø12 | 2 | Uncoated / AlCrN | – | – |
| DSF (Z2)Drills with 2 straight flutes | Ø2 - Ø16 | 2 | Uncoated / AlCrN | – | – |
Values are starting recommendations; adjust them to machine rigidity, clamping, tool length and coolant.
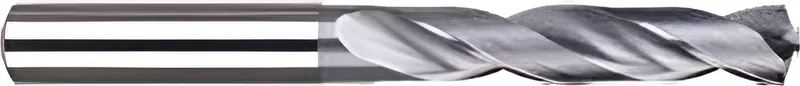
D32 Series
3xD, internal coolant

D52 Series
5xD, internal coolant

D82 Series
8xD, internal coolant
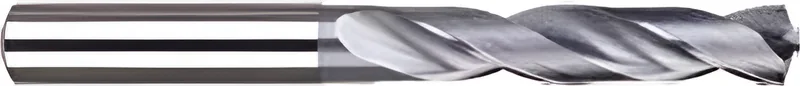
DT50 Series
5xD, internal coolant
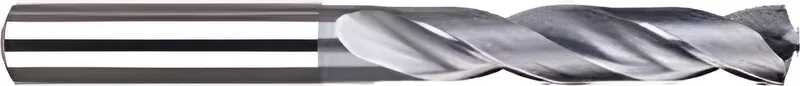
DT80 Series
8xD, internal coolant
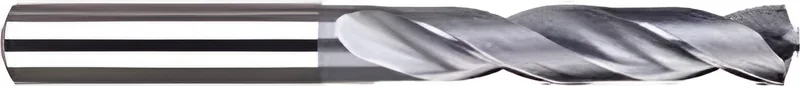
D30 Series
3xD, external coolant

D50 Series
5xD, external coolant
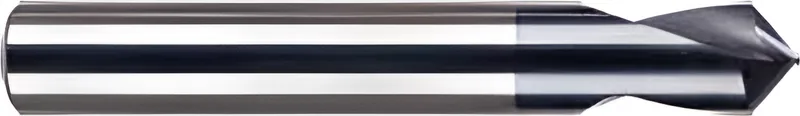
NC90 Series
NC spot drills
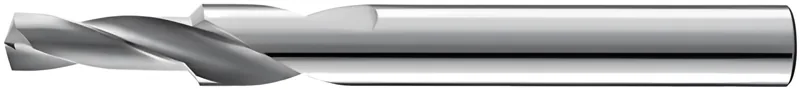
D181 Series
Short solid carbide 90° step drill
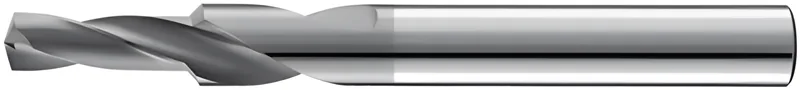
D181F Series
Short solid carbide 90° step drill
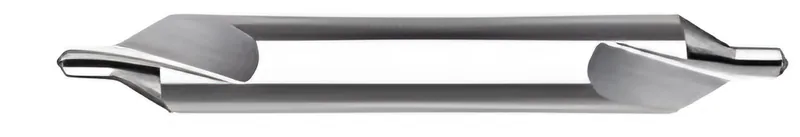
DC Series
Carbide centre drill
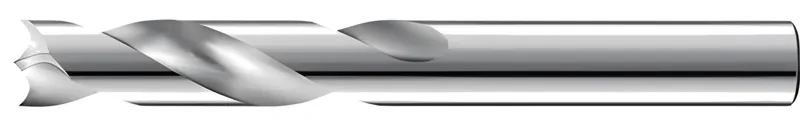
DK Series
Drills for Kevlar
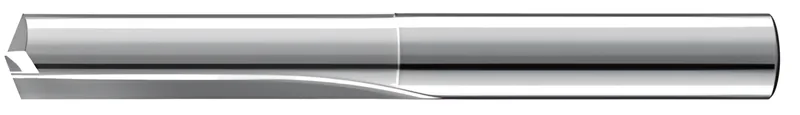
DSF Series
Drills with 2 straight flutes
Related pages
- Solid carbide drills with internal coolant
- Solid carbide reamers
- Custom carbide tools made to your drawing
- Carbide end mill (solid carbide) series – Geppetto Cutting Tools
- Technical article: Internal Coolant Carbide Drills: How to Choose and Use 3xD, 5xD and 8xD Drills
- End mill speed and feed calculator (Vc to RPM)
- Regrinding
- Technical article: Carbide Tool Regrinding Guide: When to Regrind End Mills and Drills, How Often, and Why Recoat
- All Carbide Drills
Frequently asked questions
Which series are suitable for carbide drills?
Our catalogue has 13 series for this application: D32 (Z2), D52 (Z2), D82 (Z2), DT50 (Z2), DT80 (Z2), D30 (Z2), D50 (Z2), NC90 (Z2), D181 (Z2), D181F (Z2), DC (Z2), DK (Z2), DSF (Z2). Overall diameter range: Ø0.5–Ø20 mm.
Which coatings are available in these series?
The series on this page are available with: AlTiN (high heat resistance), Uncoated, AlCrN (wear resistance).
What is the difference between a carbide drill and an HSS drill?
A carbide drill is much harder than HSS and keeps cutting ability at higher temperatures. That means higher cutting speed and feed with longer life – but it needs rigid holding and low runout.
Which carbide drills have internal coolant?
D32 (3xD), D52 (5xD) and D82 (8xD) Ø3–Ø20, and DT50 and DT80 Ø1–Ø2.9, have internal coolant. D30 and D50 are external coolant.
Do you make non-standard diameters or step carbide drills?
Yes. From your drawing or dimensioned sketch we make step and special-profile carbide drills; diameter, step length, point angle and coating follow your application.
How do I get a quote or send a drawing?
Use the “Get a quote / Send a drawing” section on this page to write to us on WhatsApp (+90 537 777 96 44) or by e-mail (info@geppetto-tr.com); you can attach your drawing. The product or page name is added to your message automatically. You can also use the quote form.
Get a quote / Send a drawing
Subject: Carbide drill series – Geppetto Cutting Tools. Message us on WhatsApp or by e-mail and attach your drawing or a dimensioned sketch. The product/page name is added automatically – just add material, size and quantity.
- 1Drawing or dimensions
- 2Material and quantity
- 3Quote and feasibility reply