
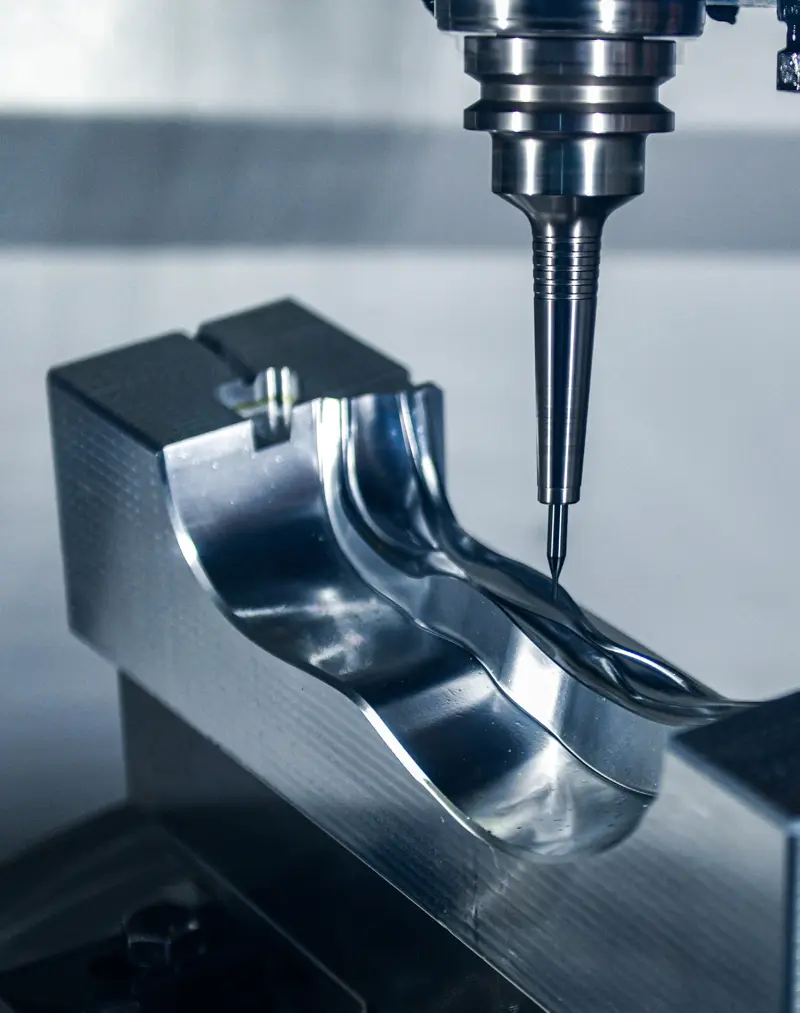
Carbide end mills for stainless steel
The solid carbide end mill series in our catalogue recommended for stainless steel (ISO M) – diameter, flutes, coating, hardness limit and 2026 catalogue cutting data in one table.
The right end mill for stainless steel depends on the operation (slotting, side milling, roughing), the reach required and the hardness of the part. The series below are the Geppetto end mills whose application range includes stainless steel. Each row links to the product page with full dimension tables and cutting data.
Quick selection guide
- General slotting and side milling: MS series (Z2, Z3, Z4) and the MR corner-radius series.
- High metal removal: MC, MC (Z4) and serrated MRS roughing end mills.
- Deep pockets and tall walls: MLR, MSXM, MCL, MCX and MRC long-neck series.
- Polished version: MPR series.
Get a quote / Send a drawing
Subject: Carbide end mills for stainless steel. Message us on WhatsApp or by e-mail and attach your drawing or a dimensioned sketch. The product/page name is added automatically – just add material, size and quantity.
- 1Drawing or dimensions
- 2Material and quantity
- 3Quote and feasibility reply
Compare the series
| Series | Diameter | Z | Coating | Helix angle | Hardness | Cutting data · ISO M |
|---|---|---|---|---|---|---|
| MS (Z2)Plain cutting edge, standard length | Ø3 - Ø20 | 2 | AlTiN | 35° | <48 HRC | Vc (m/min): 60–170 fz (mm/tooth): 0.003–0.18 |
| MS (Z3)Plain cutting edge, standard length | Ø3 - Ø20 | 3 | AlTiN | 35° | <48 HRC | Vc (m/min): 60–170 fz (mm/tooth): 0.003–0.18 |
| MS (Z4)Plain cutting edge, standard length | Ø3 - Ø20 | 4 | AlTiN | 35° | <48 HRC | Vc (m/min): 60–170 fz (mm/tooth): 0.003–0.18 |
| MR (Z4)Corner radius, standard length | Ø3 - Ø20 | 4 | AlTiN | 35° | <48 HRC | – |
| MPR (Z4)Plain cutting edge, polished | Ø3 - Ø20 | 4 | AlTiN | 35° | <48 HRC | n (rpm): 1100–14000 Vf (mm/min): 260–1060 |
| MLR (Z4)Long reach, corner radius | Ø3 - Ø16 | 4 | AlTiN | 35° | <48 HRC | – |
| MSXM (Z4)Extra long | Ø3 - Ø20 | 4 | AlCrN | 35° | <48 HRC | n (rpm): 1100–14000 Vf (mm/min): 260–1060 |
| MC (Z4)High-performance roughing end mills | Ø6 - Ø20 | 4 | AlCrN | ~45° | <56 HRC | – |
| MC (Z6)High-performance roughing end mills | Ø6 - Ø20 | 6 | TiSiN | ~45° | <56 HRC | – |
| MRS (Z4)Serrated (chip-breaker) roughing end mills | Ø6 - Ø20 | 4 | AlCrN | ~45° | <56 HRC | Vc (m/min): 60–170 fz (mm/tooth): 0.006–0.36 |
| MRS (Z6)Serrated (chip-breaker) roughing end mills | Ø6 - Ø20 | 6 | AlCrN | ~45° | <56 HRC | Vc (m/min): 60–170 fz (mm/tooth): 0.006–0.36 |
| MCL (Z4)Long neck roughing end mills | Ø3 - Ø16 | 4 | AlTiN | ~45° | <56 HRC | – |
| MCL (Z6)Long neck roughing end mills | Ø6 - Ø20 | 6 | TiSiN | ~45° | <56 HRC | – |
| MCX (Z4)Extra long roughing end mills | Ø3 - Ø12 | 4 | AlTiN | ~45° | <56 HRC | – |
| MRC (Z4)Long reach roughing, corner radius | Ø6 - Ø20 | 4 | TiSiN | ~45° | <56 HRC | – |
| MF1C (Z4)Coated end mills for general use | Ø3 - Ø12 | 4 | AlCrN | – | – | Vc (m/min): 80–150 fz (mm/tooth): 0.012–0.08 |
Values are starting recommendations; adjust them to machine rigidity, clamping, tool length and coolant.
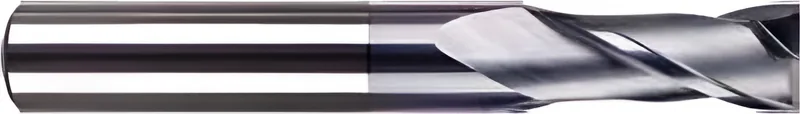
MS Series (Z2)
Plain cutting edge, standard length
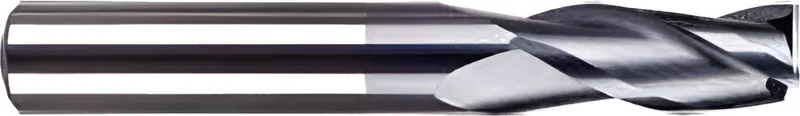
MS Series (Z3)
Plain cutting edge, standard length
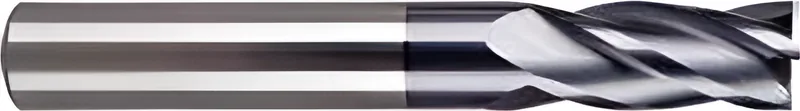
MS Series (Z4)
Plain cutting edge, standard length
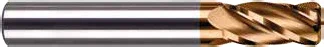
MR Series
Corner radius, standard length
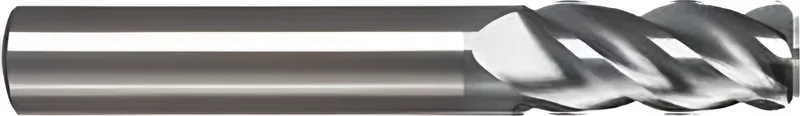
MPR Series (Z4)
Plain cutting edge, polished
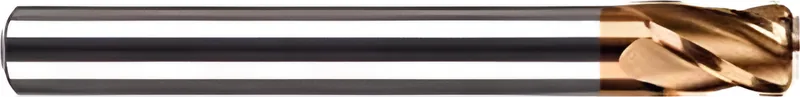
MLR Series (Z4)
Long reach, corner radius
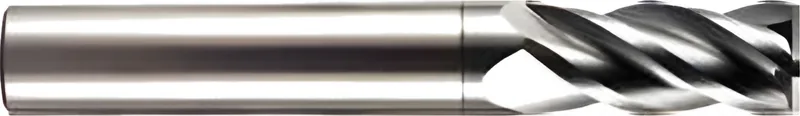
MSXM Series (Z4)
Extra long
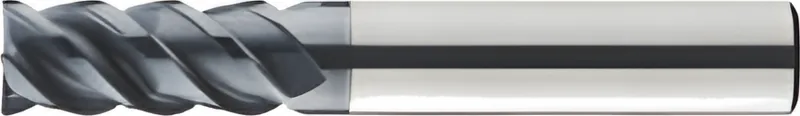
MC Series (Z4)
High-performance roughing end mills
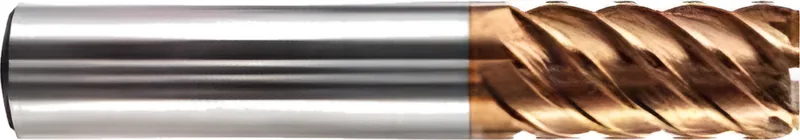
MC Series
High-performance roughing end mills
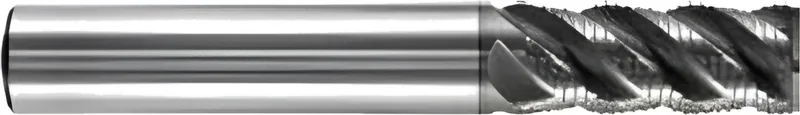
MRS Series (Z4)
Serrated (chip-breaker) roughing end mills
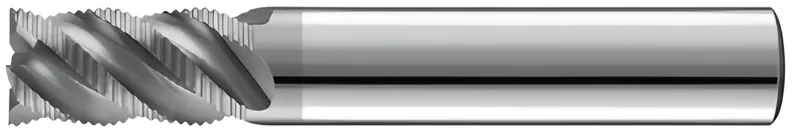
MRS Series (Z6)
Serrated (chip-breaker) roughing end mills
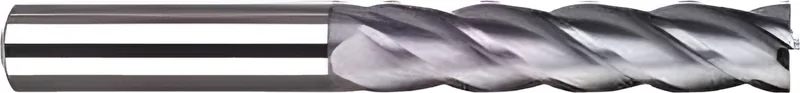
MCL Series (Z4)
Long neck roughing end mills
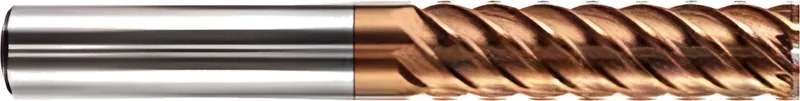
MCL Series (Z6)
Long neck roughing end mills

MCX Series
Extra long roughing end mills

MRC Series (Z4)
Long reach roughing, corner radius
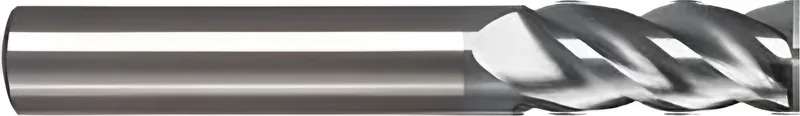
MF1C Series (Z4)
Coated end mills for general use
Short video: manufacturing and regrinding
Solid carbide end mills, D32 · D52 · D82 internal coolant drills, reamers, custom step tools and regrinding on Walter Helitronic machines – a 32-second short video.
Frequently asked questions
Which series are suitable for milling stainless steel?
Our catalogue has 16 series for this application: MS (Z2), MS (Z3), MS (Z4), MR (Z4), MPR (Z4), MLR (Z4), MSXM (Z4), MC (Z4), MC (Z6), MRS (Z4), MRS (Z6), MCL (Z4), MCL (Z6), MCX (Z4), MRC (Z4), MF1C (Z4). Overall diameter range: Ø3–Ø20 mm.
Which coatings are available in these series?
The series on this page are available with: AlTiN (high heat resistance), AlCrN (wear resistance), TiSiN (extreme hardness).
What cutting data does the catalogue give for ISO M?
According to the Product Catalogue 2026 tables (min–max): MS (Z2): Vc (m/min) 60–170, fz (mm/tooth) 0.003–0.18; MS (Z3): Vc (m/min) 60–170, fz (mm/tooth) 0.003–0.18; MS (Z4): Vc (m/min) 60–170, fz (mm/tooth) 0.003–0.18; MRS (Z4): Vc (m/min) 60–170, fz (mm/tooth) 0.006–0.36; MRS (Z6): Vc (m/min) 60–170, fz (mm/tooth) 0.006–0.36; MF1C (Z4): Vc (m/min) 80–150, fz (mm/tooth) 0.012–0.08. Values are starting recommendations; adjust them to your machine, clamping and coolant.
Up to what hardness can these series be used?
Hardness limits in the catalogue: <48 HRC: MS (Z2), MS (Z3), MS (Z4), MR (Z4), MPR (Z4), MLR (Z4), MSXM (Z4); <56 HRC: MC (Z4), MC (Z6), MRS (Z4), MRS (Z6), MCL (Z4), MCL (Z6), MCX (Z4), MRC (Z4).
How do I calculate speeds and feeds for stainless steel?
Enter the Vc and fz values from the table into our cutting data calculator to get spindle speed (n) and feed rate (Vf) for your diameter.
How do I get a quote or send a drawing?
Use the “Get a quote / Send a drawing” section on this page to write to us on WhatsApp (+90 537 777 96 44) or by e-mail (info@geppetto-tr.com); you can attach your drawing. The product or page name is added to your message automatically. You can also use the quote form.
Get a quote / Send a drawing
Subject: Carbide end mills for stainless steel. Message us on WhatsApp or by e-mail and attach your drawing or a dimensioned sketch. The product/page name is added automatically – just add material, size and quantity.
- 1Drawing or dimensions
- 2Material and quantity
- 3Quote and feasibility reply