
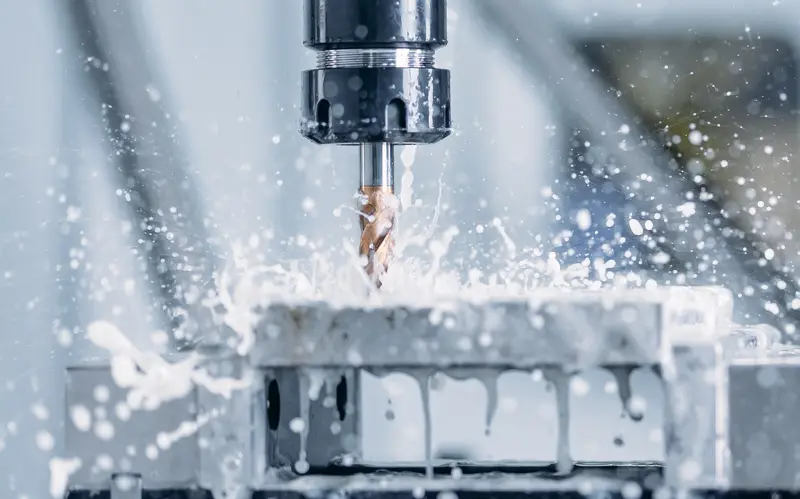
Solid carbide drills with internal coolant
Solid carbide drills that deliver coolant through the tool to the cutting zone: 3xD, 5xD and 8xD lengths from Ø1 to Ø20, AlTiN coated, with 2026 catalogue cutting data.
With internal coolant drills, the coolant flows through the tool to the drill point – which helps chip evacuation, especially in deeper holes. Geppetto internal coolant series are made in 3xD, 5xD and 8xD lengths according to hole depth; for small diameters the DT series start at Ø1.
Quick selection guide
- 3xD: D32 series, Ø3–Ø20.
- 5xD: D52 (Ø3–Ø20) and DT50 (Ø1–Ø2.9).
- 8xD: D82 (Ø3–Ø20) and DT80 (Ø1–Ø2.9).
- No internal coolant on your machine: D30 and D50 external coolant series.
Get a quote / Send a drawing
Subject: Solid carbide drills with internal coolant. Message us on WhatsApp or by e-mail and attach your drawing or a dimensioned sketch. The product/page name is added automatically – just add material, size and quantity.
- 1Drawing or dimensions
- 2Material and quantity
- 3Quote and feasibility reply
Compare the series
| Series | Diameter | Z | Coating | Cutting data · ISO P | Cutting data · ISO M |
|---|---|---|---|---|---|
| D32 (Z2)3xD, internal coolant | Ø3 - Ø20 | 2 | AlTiN | Vc (m/min): 20–180 fn (mm/rev): 0.015–0.44 | Vc (m/min): 35–105 fn (mm/rev): 0.035–0.38 |
| D52 (Z2)5xD, internal coolant | Ø3 - Ø20 | 2 | AlTiN | Vc (m/min): 20–180 fn (mm/rev): 0.015–0.44 | Vc (m/min): 35–105 fn (mm/rev): 0.035–0.38 |
| D82 (Z2)8xD, internal coolant | Ø3 - Ø20 | 2 | AlTiN | Vc (m/min): 30–150 fn (mm/rev): 0.04–0.43 | Vc (m/min): 20–60 fn (mm/rev): 0.04–0.24 |
| DT50 (Z2)5xD, internal coolant | Ø1 - Ø2.9 | 2 | AlTiN | Vc (m/min): 10–145 fn (mm/rev): 0.008–0.44 | Vc (m/min): 25–85 fn (mm/rev): 0.04–0.38 |
| DT80 (Z2)8xD, internal coolant | Ø1 - Ø2.9 | 2 | AlTiN | Vc (m/min): 10–145 fn (mm/rev): 0.008–0.44 | Vc (m/min): 25–85 fn (mm/rev): 0.04–0.38 |
Values are starting recommendations; adjust them to machine rigidity, clamping, tool length and coolant.
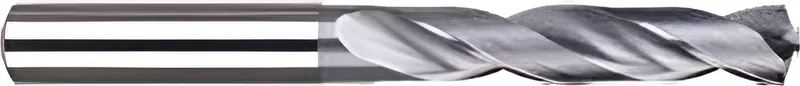
D32 Series
3xD, internal coolant

D52 Series
5xD, internal coolant

D82 Series
8xD, internal coolant
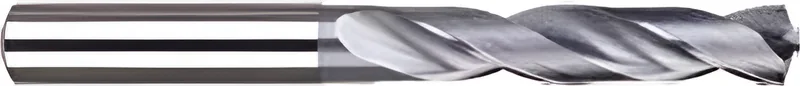
DT50 Series
5xD, internal coolant
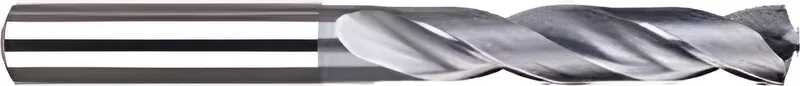
DT80 Series
8xD, internal coolant
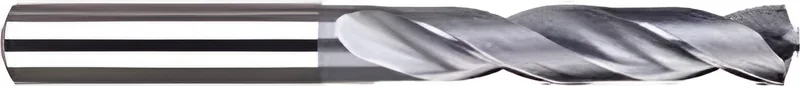
D30 Series
3xD, external coolant

D50 Series
5xD, external coolant
Short video: manufacturing and regrinding
Solid carbide end mills, D32 · D52 · D82 internal coolant drills, reamers, custom step tools and regrinding on Walter Helitronic machines – a 32-second short video.
Frequently asked questions
Which series are suitable for through-coolant drilling?
Our catalogue has 5 series for this application: D32 (Z2), D52 (Z2), D82 (Z2), DT50 (Z2), DT80 (Z2). Overall diameter range: Ø1–Ø20 mm.
Which coatings are available in these series?
The series on this page are available with: AlTiN (high heat resistance).
What cutting data does the catalogue give for ISO P?
According to the Product Catalogue 2026 tables (min–max): D32 (Z2): Vc (m/min) 20–180, fn (mm/rev) 0.015–0.44; D52 (Z2): Vc (m/min) 20–180, fn (mm/rev) 0.015–0.44; D82 (Z2): Vc (m/min) 30–150, fn (mm/rev) 0.04–0.43; DT50 (Z2): Vc (m/min) 10–145, fn (mm/rev) 0.008–0.44; DT80 (Z2): Vc (m/min) 10–145, fn (mm/rev) 0.008–0.44. Values are starting recommendations; adjust them to your machine, clamping and coolant.
What cutting data does the catalogue give for ISO M?
According to the Product Catalogue 2026 tables (min–max): D32 (Z2): Vc (m/min) 35–105, fn (mm/rev) 0.035–0.38; D52 (Z2): Vc (m/min) 35–105, fn (mm/rev) 0.035–0.38; D82 (Z2): Vc (m/min) 20–60, fn (mm/rev) 0.04–0.24; DT50 (Z2): Vc (m/min) 25–85, fn (mm/rev) 0.04–0.38; DT80 (Z2): Vc (m/min) 25–85, fn (mm/rev) 0.04–0.38. Values are starting recommendations; adjust them to your machine, clamping and coolant.
What does my machine need for internal coolant drills?
A machine or holder that supplies coolant through the tool (through-spindle coolant). If you do not have it, use our D30 (3xD) and D50 (5xD) external coolant series.
How do I get a quote or send a drawing?
Use the “Get a quote / Send a drawing” section on this page to write to us on WhatsApp (+90 537 777 96 44) or by e-mail (info@geppetto-tr.com); you can attach your drawing. The product or page name is added to your message automatically. You can also use the quote form.
Get a quote / Send a drawing
Subject: Solid carbide drills with internal coolant. Message us on WhatsApp or by e-mail and attach your drawing or a dimensioned sketch. The product/page name is added automatically – just add material, size and quantity.
- 1Drawing or dimensions
- 2Material and quantity
- 3Quote and feasibility reply